If you’ve ever relied on trunnion mounted ball valves to keep your oil and gas, chemical processing, power generation, or water treatment lines running without a hitch, you know these components are the unsung heroes of industrial piping. Unlike their floating ball counterparts, trunnion valves are designed with axial support for the ball, which lets them handle higher pressures, larger flow rates, and more extreme operating conditions—all without warping or leaking. But here’s the thing: even the most robust trunnion ball valves won’t perform at their best if you skip regular maintenance. As a supplier that’s worked with operators across heavy industry for over a decade, I’ve seen firsthand how small, consistent upkeep can extend a valve’s lifespan by years, while cutting unplanned downtime and emergency repair costs. Today, I’m breaking down exactly what maintenance your trunnion valves need, when to do it, and why it matters for your bottom line. Trunnion Mounted Ball Valves
First, let’s get clear on one thing: trunnion ball valve maintenance isn’t a one-size-fits-all task. The needs of a valve in a high-pressure hydrogen service plant are very different from one in a municipal water treatment facility, and a valve in a cold-weather refinery will face far different stresses than one in a desert desalination plant. But regardless of your application, there are core maintenance steps that apply to every trunnion mounted ball valve, paired with checks tailored to your operating environment. I always tell clients to think of trunnion valve maintenance in two buckets: routine, scheduled tasks you can do without shutting down your full line, and more thorough, periodic inspections that require partial or full line isolation.
Starting with the routine daily and weekly checks—these are the quick, low-labor steps that catch issues before they turn into failures. The first thing you should do every time you walk by a valve: run a visual inspection of the actuator and valve body. Look for any signs of seepage around the stem or valve body joints. A tiny dribble of fluid that goes unnoticed can corrode the stem threads or seat surfaces over time, leading to full leakage later. For manually operated valves, check the handwheel or lever for signs of sticking when you open or close the valve. If it feels stiff, that’s a warning that the stem isn’t moving smoothly, which can strain the valve’s internal components. For actuator-driven valves (pneumatic, electric, or hydraulic), listen for unusual clicking or grinding during cycling—those noises usually mean the actuator isn’t aligned properly or the stem is catching on debris.
Once a month, I recommend pulling a bit more data on each valve’s performance. Log the number of times it cycles (opening and closing) and compare it to the baseline number when the valve was first installed. If it’s cycling more often than expected, that could mean there’s a leak upstream or downstream that’s forcing the valve to compensate, or the internal seals are wearing out and causing pressure buildup. For valves in hazardous fluid service, check the air supply to pneumatic actuators, or the power connections for electric actuators, to make sure they’re running at the correct pressure or voltage. Even a 10% drop in pneumatic pressure can make a valve only partially open or close, which will cause erosion of the ball and seat surfaces over time.
Now, moving to the more involved periodic maintenance—these tasks are usually done every six months to two years, depending on your operating conditions, and require isolating the valve, draining the line, and accessing the internal components. The most critical part of a trunnion valve is its seat and ball assembly, because that’s what creates the seal that prevents leakage. Unlike floating ball valves, trunnion valves use spring-loaded seats that press against the ball, so regular lubrication and seat inspections are non-negotiable.
Lubrication is a big one, and I can’t tell you how many operators either over-lubricate or under-lubricate their trunnion valves. Over-lubrication can cause built-up grime to get trapped between the ball and seats, leading to sticking and wear. Under-lubrication, though, means the seats and stem can’t move smoothly, leading to increased friction and pressure on the trunnion bearings. The right approach: use the lubricant recommended by your valve manufacturer (not just any generic industrial grease). For most trunnion valves, we supply a food-grade, high-pressure synthetic lubricant that works in temperatures from -40°F to 350°F, and it’s designed to not react with the process fluids common in oil and gas and chemical processing. Every six months, inject a small amount of lubricant through the grease fitting on the valve—usually just 10 to 15 grams, depending on the valve size. If you notice old, dirty grease coming out of the vent fitting while you inject, that’s a sign you need to clean the fitting and lines before adding fresh lubricant, to avoid pushing contaminants into the valve body.
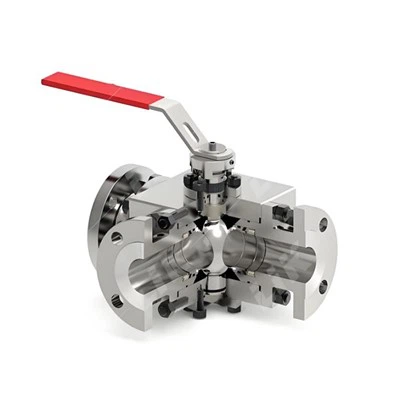
When you do open a valve for periodic inspection, the first thing to check is the ball and seat surfaces for signs of wear, corrosion, or scoring. Scoring is a common issue in valves handling abrasive fluids like sand-laden crude oil or mineral slurries—small scratches on the ball or seat can create gaps that lead to leakage. If the scratches are deeper than 0.5mm, you’ll need to replace the seats; smaller scratches can usually be polished out with a non-abrasive compound, as long as you don’t damage the ball’s precision surface (the ball on a trunnion valve is machined to within microns of perfect roundness, so even a tiny nick can ruin the seal). Also, check the trunnion bearings—these are the small, heavy-duty bearings that support the ball from below and above, taking the full weight of the process pressure. If you hear grinding or feel play when you rotate the ball by hand, the bearings are worn and need to be replaced.
Another key internal check is the valve’s body and bonnet for corrosion. Even in mild applications, valves can develop pitting over time from moisture or process chemicals. If you notice any deep pits on the valve body walls, that’s a sign the valve is at risk of failure, especially in high-pressure service. If the pits are minor, you can have the valve reconditioned, but if they’re deep enough to weaken the body, you’ll need to replace it. I always advise clients to keep a spare set of seats and trunnion bearings on hand for each valve in critical service—waiting three days for a replacement seat can cost tens of thousands of dollars in lost production.
There are also environment-specific maintenance steps that you can’t skip, depending on where your valve is operating. For valves in cold climates (temperatures below 32°F), make sure to insulate the valve body and actuator to prevent process fluids from freezing. Frozen fluids can expand and crack the valve body, or jam the ball so it breaks when you try to open it. I’ve had a client in northern Canada lose a full refinery line because a valve’s stem froze solid, and they tried to force it open, snapping the stem and causing a major leak—all because they skipped insulating the valve in winter. For valves in hot, humid environments (like coastal refineries), you’ll need to inspect the valve’s external coating every three months for signs of peeling or corrosion, and reapply coating as needed to prevent rust from eating through the body. For valves handling abrasive fluids, you can increase the frequency of seat inspections to every three months, since the abrasive particles will wear down the seats much faster than in clean water or gas service.
One common mistake I see many operators make is waiting until the valve is leaking to do maintenance. By the time you see a leak around the stem or body, the seats have already worn down enough that the ball is damaged, and the trunnion bearings may be on their last legs. Instead, use the valve’s cycling data and pressure readings to catch issues early. For example, if you notice that the differential pressure across the valve increases when it’s closed, that’s a sign the seat seal is leaking, so you can schedule maintenance during a planned shutdown, rather than an emergency repair.
Let me also talk about testing after maintenance, because it’s just as important as the maintenance itself. Once you’ve completed any routine or periodic work, you need to test the valve to make sure it’s working correctly. The first test is a visual and pressure test: pressurize the valve on both sides (or isolate one side) and check for seepage around the stem and body. If there’s no seepage, you’re good. The second test is a cycling test: open and close the valve 10 times, checking that it moves smoothly, and that the actuator reaches full open and full close position without sticking. For valves in hazardous service, you may also want to do a leak test with a tracer gas, to catch any tiny leaks that aren’t visible to the naked eye.
At the end of the day, trunnion mounted ball valves are designed for long life, but only if you treat them with consistent, targeted maintenance. As a supplier, I’ve seen clients that follow a strict maintenance schedule cut their valve-related downtime by 70%, compared to those that only do maintenance when something breaks. This isn’t about overcomplicating your operations—it’s about small, regular steps that keep your most critical components running smoothly. If you’re unsure about the specific maintenance schedule for your trunnion valves, or you need help inspecting your existing valves to identify potential issues, I’m here to help. Whether you need replacement parts, on-site inspection services, or advice tailored to your specific application, you can reach out to our team to discuss your needs. Don’t wait until a valve fails to protect your operations—start a maintenance plan today to keep your lines running reliably for years to come.
Actuator REFERENCES
- Hydraulic Institute. (2020). Pump and Valve Maintenance Handbook: Trunnion Mounted Ball Valves. Hydraulic Institute Press.
- American Petroleum Institute. (2019). API 6D: Specification for Pipeline Valves. 2nd Edition.
- Ball Valve Manufacturers Association. (2021). Best Practices for Trunnion Ball Valve Maintenance. BVMA Technical Report Series.
- International Society of Automation. (2020). Field Maintenance Guidelines for Industrial Valves, Part 2: Trunnion Mounted Designs. ISA-75.01.05.
- Materials Performance and Corrosion Center. (2022). Corrosion Mitigation Strategies for Trunnion Ball Valves in Harsh Process Environments. MPCC Technical Bulletin.
Wuxi PYNOS Flow-tech Co., Ltd.
As one of the leading trunnion mounted ball valves manufacturers and suppliers in China, we offer a wide range of products with superior quality. We warmly welcome you to buy high quality trunnion mounted ball valves made in China here from our factory. We also accept customized orders.
Address: Sales Center: 7th Floor, No.19 Qingyuan RD, Wuxi City, Jiangsu Prov., China
E-mail: Info@pynosvalve.com
WebSite: https://www.pynosvalves.com/
