If you’re reading this, chances are you own a hydraulic surface grinder (or are thinking of picking one up from a reputable supplier) and have found yourself asking: “Wait, why is my table moving way too fast for this fine grinding pass, or way too slow when I should be cranking through rough cuts?” Let’s cut to the chase—adjusting that table speed isn’t just a “turn a dial” trick. It’s tied to how your grinder’s hydraulic system works, and getting it right makes parts better, your machine last longer, and saves you from burning out or ruining workpieces. I’ve been in the surface grinder game for over a decade, so I’ve seen every mistake under the sun (from new fabricators cranking the speed to test limits to seasoned operators forgetting a simple check). Let’s break this down like we’re chatting over a coffee at the trade show floor—no stuffy jargon, just real, usable steps. Hydraulic Surface Grinder

First, let’s make sure we’re on the same page: hydraulic surface grinders don’t use those cheap rack-and-pinion systems like older manual grinders. The table glides on pressurized hydraulic fluid, and that’s where speed is controlled. Most people think the speed dial is the only control, but there’s a whole system under the hood that relies on pressure, fluid level, and even wear and tear. Before you touch any dials, do your pre-checks. I can’t tell you how many times I’ve gotten a panicked call from a customer saying their table is stuck or lurching, and it’s just because they didn’t top off the hydraulic fluid. Low fluid levels cause air bubbles to get sucked into the lines, which messes with pressure regulation and makes speed jump around like a squirrel on a hot tin roof.
Next, check the fluid condition. If your fluid is dark, gritty, or smells burnt, that’s a problem. Contaminated fluid clogs the flow control valves that adjust table speed, so even if you turn the dial, you won’t get a consistent speed. I always tell my customers: change your hydraulic fluid every 1,000 operating hours, and add a filter upgrade if you’re grinding with abrasive materials that generate lots of metal shavings. That small step alone will make speed adjustments way smoother.
Now, let’s get into the actual adjustment steps. First, identify your machine’s speed control components. Most mid-range to high-end hydraulic surface grinders have two main speed controls: a coarse adjust (usually a big knob or lever for rough grinding) and a fine adjust (a smaller dial for precision passes). Some budget models only have a single knob, but the logic still applies. Let’s start with the safety first—turn off the grinder, disconnect the power source, and make sure the wheel is not engaged. You don’t want the table lurching while you’re sticking your hand near it, trust me.
Once you’re safe, locate the flow control valve. This is the part that regulates how much hydraulic fluid flows to the table’s drive motor, which in turn sets how fast the table moves. It’s usually on the side of the machine’s hydraulic pump housing, or near the front operator panel. The coarse adjust is usually a lever that slides between “Fast” and “Slow”—don’t just yank it all the way to one side. For rough grinding (like removing heavy stock from a steel block), set the coarse adjust to the mid-fast range. Why? Rough grinding doesn’t require high precision, and moving faster here cuts down on cycle time. But if you’re working with delicate materials, like aluminum or thin workpieces, keep the coarse adjust in the mid-slow range to avoid vibration that can warp the part.
Now the fine adjust is where most people mess up. This is where you get the exact speed you need for precision passes, like finishing a surface to a flatness of 0.001mm. The fine adjust dial is usually marked with numbers or hash marks, but don’t get too hung up on those numbers—they’re just general guides. Here’s my go-to trick: run the grinder on a dry run (no workpiece, just the table moving) first. Turn on the power, set the coarse adjust to where you think you need it, then slowly tweak the fine adjust. Watch how the table moves—if it’s creeping too slow, turn the dial clockwise to open the flow valve more (more fluid = faster table). If it’s too fast, turn it counterclockwise to restrict flow. Do this on a dry run first so you don’t waste material if you get the speed wrong later.
Wait, there’s another hidden setting some people miss: the pressure relief valve. This is a safety feature that prevents the hydraulic system from getting too much pressure, which can damage the pump or cause the table to lurch. If you’ve adjusted the flow control and the table is still inconsistent, check the pressure gauge on the pump housing. For most surface grinders, the operating pressure should be between 500 and 1,200 PSI, depending on the model. If it’s higher than that, the pressure relief valve is probably stuck or set too high, which will make the table speed jump. Adjusting the pressure relief valve is a bit more hands-on—you’ll need a wrench to turn the set screw on the valve, but I recommend checking your machine’s manual first, or calling us if you’re not comfortable. It’s not rocket science, but you don’t want to break a $1,000 valve because you guessed wrong.
Another thing to consider: the type of grinding you’re doing. I see a lot of operators use the same speed for every job, and that’s a surefire way to get bad parts. For surface grinding, table speed is tied to the “feed rate,” which is how much material the grinding wheel removes per pass. Let’s make this simple: if you’re grinding a hard material like tool steel, you need a slower table speed. Hard materials generate more heat, so moving slower gives the wheel time to cut into the material evenly without burning the workpiece (burnt steel is ruined, trust me, I’ve had customers send me parts that look like they were charred on a campfire because they ran too fast on tool steel). For softer materials like brass or plastic, you can crank the table a bit faster—they don’t generate as much heat, so you can move quicker to get the job done.
Wait, what if you have a variable frequency drive (VFD) on your grinder? More and more modern hydraulic surface grinders have these instead of traditional flow control valves, and they’re way easier to adjust. VFDs control the speed of the electric motor that drives the hydraulic pump, so instead of turning a valve, you just input a speed percentage on the control panel. For these machines, the same rule applies: slower speed for hard materials, faster for soft, but you have a lot more precision. I recommend setting the VFD speed based on the wheel’s diameter—if your wheel is new (larger diameter), you might need a slightly slower speed than if the wheel is worn down. That’s because a bigger wheel covers more distance per rotation, so the table has to move slower to keep the feed rate consistent.
Now, common mistakes I see all the time: First, adjusting the speed while the grinder is running at full load. If you have a workpiece clamped down and the wheel is engaged, adjusting the flow control can cause the table to lurch, which might damage the workpiece or even throw it off the chuck. Always do speed adjustments on a dry run, or when the wheel is not touching the workpiece. Second, ignoring maintenance. I mentioned fluid level earlier, but also check the flow control valve’s o-rings. If o-rings are worn, they leak hydraulic fluid, which causes pressure drops and inconsistent speed. That’s a cheap fix—o-rings cost a few bucks, and it takes 10 minutes to replace them. Third, comparing speed to other machines. Every hydraulic surface grinder is a little different, even from the same brand. Your machine’s age, how well it’s maintained, and the condition of the pump will all affect how speed translates to movement. Don’t worry about what the guy next to you is doing—focus on what works for your machine and your parts.
If you’re still having trouble after trying these steps, that’s totally fine. I’ve been in this long enough to know that sometimes small, hard-to-spot issues (like a clogged filter or a worn piston in the hydraulic motor) mess with speed. That’s why our team offers free support for every machine we sell—we don’t just drop a grinder at your shop and ghost you. If you’re in the market for a new hydraulic surface grinder, or you need help troubleshooting the one you have, don’t hesitate to reach out. We can walk you through adjustments over the phone, or even send a technician to your shop if it’s something more complex. Adjusting table speed is one of the most important skills for a surface grinder operator, and getting it right will make your work faster, better, and less frustrating.
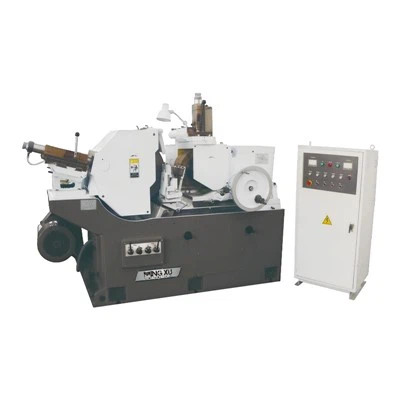
At the end of the day, it’s all about balance. You don’t want to go too fast and burn parts or damage your machine, and you don’t want to go too slow and waste time. Take the time to check your fluid, do dry runs, and adjust for the material you’re working with, and you’ll be a pro in no time. If you’re ready to upgrade your setup or get a reliable hydraulic surface grinder that’s easy to adjust and maintain, just connect with our team—we’d be stoked to help you find the right fit for your shop.
Hydraulic Surface Grinder References:
- Machine Tool Hydraulics: Operation, Maintenance, and Troubleshooting, 3rd Edition, Society of Manufacturing Engineers, 2018
- Surface Grinding Technology: Principles and Practice, Woodhead Publishing, 2020
- Hydraulic System Maintenance Best Practices, Fluid Power Industry Association, 2021
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional hydraulic surface grinder manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best hydraulic surface grinder for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
