If you’ve ever stood in a facility where an induction furnace hums through its melt cycle, you know the focus often lands on the fiery, liquid metal pool and the precision of the power controls. But if you ask anyone who’s spent decades in metallurgical parts supply like I have, they’ll tell you the unglamorous, hardworking slag removal section of that furnace is one of the most critical, underrated components in the entire setup. For anyone sourcing parts for induction furnaces—whether you’re running a small foundry or a large-scale steel production plant—understanding exactly what this section does isn’t just technical trivia; it’s the difference between a smooth, cost-effective melt and a catastrophic, production-stopping delay. Let me break this down from the perspective of someone who’s shipped induction furnace components to foundries across three continents, because this isn’t just textbook science—it’s what keeps their operations running, and my business running, too. Parts Of Induction Furnace
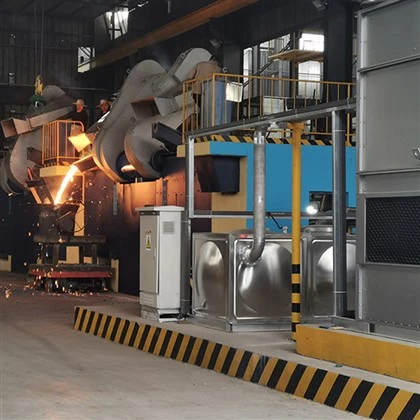
First, let’s ground this in what slag actually is, because you can’t understand the purpose of removing it without knowing what you’re dealing with. When an induction furnace heats metal (be it steel, aluminum, copper, or even specialty alloys), small impurities from the raw metal feed, the furnace lining, and the surrounding air react with each other to form a byproduct: slag. Think of it as a layer of crumbly, often glassy or semi-solid stuff that floats on top of the molten metal, since it’s less dense than the liquid metal below. At its most basic, slag is made of oxidized metals, silica, alumina, sulfur, and other non-metallic inclusions. Now, some new operators might think, “It’s just gunk, why does it matter?” But I’ve seen firsthand what happens when you ignore that gunk. Last year, a small foundry in Ohio ordered a replacement slag removal assembly from my team because their old one had worn out, and they were trying to scrape slag off manually with a hand tool during their melt cycle. By the time they ordered the new part, they’d already had three batches of billets rejected for “porosity defects”—tiny air or impurity pockets that made the metal unfit for automotive parts. The root cause? That leftover slag was seeping into the molten metal as it cooled, and their manual method couldn’t remove it fast enough without chilling the furnace. That’s the first core purpose of the slag removal section: it prevents impurity contamination of the final metal product.
But let’s go deeper than just product quality—there’s the furnace itself to consider. The refractory lining of an induction furnace, the heat-resistant material that lines the inside of the crucible where the metal melts, is expensive. A standard refractory lining for a 5-ton induction furnace can cost tens of thousands of dollars to replace, and the process requires draining the furnace, removing the old lining, and relining it over several days. Slag, especially if it’s high in silica or alkaline compounds, is highly corrosive to that refractory lining. When slag sits on top of the molten metal, it seeps into the tiny pores and cracks of the lining, and as the furnace cycles between heat and cool, that slag expands and contracts, wearing away the lining faster. I once had a customer in Germany who ran their furnace 24/7 for six months without addressing their slag buildup, and they had to replace their lining three months early. When they inspected the lining, the areas exposed to slag had eroded down to half their original thickness, while the sections covered by molten metal were almost untouched. The slag removal section’s job here is two-fold: it keeps slag from lingering on the lining long enough to cause corrosion, and it allows operators to clear slag immediately after a melt, so the lining cools evenly without the stress of trapped impurities.
Next, there’s operational efficiency. Induction furnaces run on precise energy inputs—you don’t want to waste a single watt, because energy costs make up 30-40% of a foundry’s total operating expenses. Slag that sits on top of the molten metal acts as an insulator. Molten metal radiates heat into the air, but a thick layer of slag traps that heat, meaning the furnace has to work harder to maintain the target temperature. I’ve done side-by-side checks for a pair of foundries in India that run identical 10-ton induction furnaces. One had a properly maintained slag removal system, the other was manually skimming. The first foundry used 12% less energy per melt cycle because they weren’t wasting heat trapped under excess slag. That’s not a small number—on an annual basis, that adds up to tens of thousands of dollars in savings. Beyond energy, slag buildup can interfere with the furnace’s tilting mechanism, which is used to pour the molten metal out of the crucible. If slag is caked around the spout or the tilting pivot, the furnace can’t tilt evenly, leading to spillage, inaccurate pour volumes, or even the need to shut down operations entirely to clear the blockage. The slag removal section, especially if it’s a powered assembly like a mechanical skimmer or a slag door with a controlled opening, clears away that buildup before it causes tilting issues.
Wait, there’s another purpose that’s often overlooked: safety. Working around molten metal is inherently dangerous, and anything that reduces contact between workers and hot, liquid material is a win. Manual slag removal means leaning over a furnace that’s 1,500°C (2,700°F) or more, using heavy tools that can slip and cause burns or splashes of molten metal. The slag removal section—whether it’s a robotic skimmer, a hydraulically operated slag door, or a powered rake that works from the safety of the control room—eliminates that direct contact. I remember a time when I first started working with induction furnace parts, back in the early 2000s, a fellow supplier told me about a customer whose operator suffered third-degree burns when a hand tool slipped into the molten metal while skimming slag. That accident shut down production for two weeks, and the operator was out of work for months. Investing in a reliable slag removal section isn’t just about parts—it’s about protecting the people who operate the equipment. That’s a purpose that isn’t listed in every metallurgy textbook, but it’s one I hear about from customers more than any other.
Let’s talk about the different types of slag removal sections, because their purpose varies a bit based on the design, but the core goals stay the same. For small, batch-style induction furnaces (common in job shops that make custom metal parts), a simple manually operated slag door or a powered rake is standard. For larger, continuous or semi-continuous furnaces used in mass production, you’ll find mechanical skimmers, electromagnetic slag separators, or even gas-assisted systems that blow a thin layer of air to lift slag off the metal surface. Electromagnetic separators, for example, work because most slag is non-conductive, while the molten metal is conductive. So when you run a small electromagnetic field across the metal surface, the slag is repelled to the edge of the crucible, where it can be removed. That’s a newer technology, but it’s become popular because it’s gentler on the metal and removes even fine particles that manual skimming misses. No matter the design, though, every slag removal section is built to serve those four core purposes: product purity, furnace lining protection, energy efficiency, and operator safety.
I’ve seen too many customers cut corners on their slag removal parts, because they don’t see it as a “core” part like the induction coil or the power supply. But let me tell you, a poorly functioning slag removal section can cause more damage than a faulty coil. Last year, a customer in Mexico tried to save money by buying a low-cost, generic slag rake from a non-specialized parts supplier, rather than a precision-made one from our team. The rake’s tines were made of a cheap, heat-sensitive alloy that warped after just three uses, and pieces of the tines broke off and mixed into the molten metal. They had to drain the entire furnace, clean out every piece of broken tine and embedded slag, and lost two full days of production. When they contacted me, they said they’d wasted more on lost production and repair than they would have spent on a high-quality, correctly sized slag removal section in the first place. That’s why when I talk to new customers, I always emphasize that the slag removal part isn’t an afterthought—it’s a critical component that supports the entire furnace’s performance.
Another point that’s important to mention is regulatory compliance, especially for customers operating in regions with strict environmental or quality standards. For example, in the EU, foundries have to meet specific limits for metal impurities in cast parts, and excess sulfur or oxides from slag can cause a foundry to fail inspection. In the US, the Occupational Safety and Health Administration (OSHA) has strict rules about worker safety around high-temperature equipment, so having an automated slag removal system isn’t just a good idea—it can help a facility stay compliant. I worked with a customer in Turkey last year that was facing a $50,000 fine because their manual slag removal process was exposing workers to unacceptably high heat levels, per OSHA-aligned local standards. They installed our automated slag skimmer, and not only avoided the fine, but their impurity rates dropped by 8%, so their product quality scores improved, and they won two new contracts with automotive manufacturers. That’s the kind of return on investment that makes the slag removal section worth every penny, even for operations that were trying to get by on a tight budget.
Let’s circle back to something personal, because that’s how I’ve always approached working with induction furnace parts. I started in this business 22 years ago, working in my uncle’s machine shop, where we repaired and rebuilt induction furnaces for local foundries. Back then, every customer would talk about their coils and their power supplies, but no one would mention the slag rakes or the slag doors. But I noticed that the best, longest-running operations were the ones that took care of that “boring” part of the furnace. I learned to inspect every slag removal component before we shipped a part, not just check that it fit, but make sure it was made of the right heat-resistant alloy, that the rake angles were tailored to the specific crucible size, that the hydraulics (if it was a powered system) could handle the temperature and pressure of a full melt cycle. That attention to detail is what makes our parts different, and it’s why customers come back to us time and again.

If you’re reading this, chances are you’re either a foundry manager, a maintenance technician, or someone responsible for sourcing parts for induction furnaces. You know the pressure to keep melt cycles on time, keep costs down, and keep your product quality high. The slag removal section might not be the first part you think of when you’re troubleshooting a problem, but when your metal is being rejected, your lining is wearing out too fast, your energy bills are going up, or your team is dealing with safety concerns, that’s the part you’ll be kicking yourself for not paying more attention to. At the end of the day, the purpose of the induction furnace’s slag removal part is simple: it protects your product, protects your equipment, protects your bottom line, and protects your team. It’s the quiet workhorse that makes every other part of the furnace do its job well.
Continuous Casting Machine If you’re looking to upgrade your existing slag removal system, replace worn parts, or just talk through the best setup for your specific induction furnace needs, I’m here to help. We work with operations of all sizes, from small job shops with 1-ton furnaces to large steel mills with 50-ton units, and our parts are built to last through thousands of melt cycles. Don’t wait until you’re dealing with a production shutdown or rejected batches to invest in a reliable slag removal section. Reach out to our team to discuss your requirements, and we’ll help you find the right solution for your operations.
References
- ASM International. Metallurgy of Induction Furnace Melting. ASM Handbook, Volume 15: Casting, 2008.
- Taylor, J. Industrial Furnaces: Design, Operation, and Maintenance. Elsevier, 2019.
- Occupational Safety and Health Administration (OSHA). Safety Standards for Molten Metal Operations. U.S. Department of Labor, 2021.
- European Steel Association (EUROFER). Slag Management in Ferrous Foundries. 2020.
- Gupta, S. Induction Heating: Principles and Applications. CRC Press, 2017.
Xi’an Aobang Technology Co., Ltd.
As one of the most professional parts of induction furnace manufacturers and suppliers in China, we’re featured by quality products and good price. Welcome to buy durable parts of induction furnace for sale here and get quotation from our factory. Customized orders are welcome.
Address: No.268, Caotan 6th Road, Economical and Technological Development Zone, Xi’an, Shaanxi, China.
E-mail: alicezhang@xaabfurnace.com
WebSite: https://www.xaabfurnace.com/
