If you’ve ever worked with tire manufacturing, you know the mold is where the rubber meets the road—literally. All-Steel Radial Segmented Molds (ASRSMs) are the workhorses that make the high-performance radial tires we drive on every day. But here’s the thing: a mold that’s even a hair off can throw off an entire tire’s balance, leading to uneven wear, poor fuel efficiency, or even safety issues. As a mold supplier, I get asked all the time: how do you keep these things so accurate? It’s not magic—It’s a mix of process, attention to detail, and hard-learned tricks we’ve picked up over years of doing this. Let me break it down like we’re chatting over a coffee (no stuffy industry jargon, promise). All-Steel Radial Segmented Molds
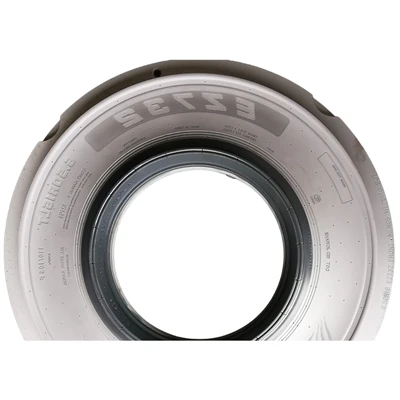
First off, let’s talk about the starting material. I can’t stress this enough—garbage in, garbage out, right? When we source the steel for our segments, we don’t just grab any bulk alloy. We use high-grade tool steel, usually P20 or H13, but we test every single batch before it even touches a machine. Last year, we had a supplier send a batch that claimed 0.002% carbon content, but our spectrometer picked up it was 0.0017%. That might sound tiny, but over the 10+ machining steps it goes through, that small difference would’ve thrown the segment’s thickness off by a few microns. Microns matter here. Like, a human hair is about 70 microns—so even a 5-micron error on a segment can add up when you have 20+ segments making up a full mold. We reject that batch, no questions, even if it means a two-week delay in production. Our customers don’t have time for molds that die prematurely or are out of spec.
Next up, the machining process. People always think we just stick a block of steel in a CNC and hit go. Nah. We use 5-axis CNC machines, but we don’t run ’em 24/7 without checking. Wait times between cuts are non-negotiable. Why? Because when steel gets heated from the spindle moving fast, it expands. If you cut a segment right when it’s warm, by the time it cools down to room temp (our shop is temperature-controlled, by the way—another must), it’ll shrink a little. So after every major pass, we let it sit for at least an hour, then use a coordinate measuring machine (CMM) to check critical dimensions: the segment’s arc, the gap where it meets the next segment, the depth of the tread grooves. Last month, we had a new machinist skip the wait time because he was behind on his quota. We caught it during a post-check, fixed it before moving to the next step, and that segment went into a mold that’s running great for a customer in Ohio. If we hadn’t checked, that tire company would’ve been down for days.
Then there’s the segmentation assembly. ASRSMs are made of individual curved segments that lock together to form a circle. The gaps between these segments—called “knife edges” or “joints”—can’t be more than 0.005 mm wide. If there’s a gap wider than that, rubber will seep in during vulcanization, leading to those annoying tiny “flash” lines on the tire. Flash isn’t just a cosmetic issue—it means the tire has to be trimmed, which slows production, and bad trimming can weaken the sidewall. How do we get those gaps so tight? We use a hand-fit process for the final joins, not just machine fitting. Our senior machinists have 15+ years of experience with this—they can feel if a segment is slightly off by running a precision feeler gauge across the joint. We also use alignment pins that are machined to exactly match each segment’s hole, so when we bolt the mold together, everything lines up perfectly. We test the mold’s roundness with a laser tracker before shipping—something most smaller suppliers skip, but it’s non-negotiable for us. A roundness error of 0.1 mm might not sound like much, but when the tire spins at 120 km/h, that translates to a wobble. No one wants a tire that shakes at highway speeds.
Heat treatment is another step that’s often overlooked, but it’s make-or-break. After machining, we harden the steel to make it durable enough to handle thousands of vulcanization cycles (each one is at 150°C and 200 psi, for reference). If we heat it too fast, or cool it unevenly, the segments warp. Warping is the enemy here. To prevent that, we use a vacuum heat treatment furnace, which heats the steel slowly and evenly in a vacuum to avoid oxidation. We also do a cryogenic treatment after hardening—cooling the segments to -180°C for 24 hours. This stabilizes the steel’s molecular structure, so it doesn’t change shape as it’s used over time. We have molds that we made 10 years ago still going strong because of this. Some competitors skip the cryo step to save time and money, but their molds start warping after 5,000 cycles, vs our molds which last 15,000+ cycles with barely any dimensional shift.
Regular maintenance for the molds themselves, when they’re in use at the customer’s plant, is a big part of keeping accuracy long-term. Wait, you might be thinking—we sell the mold, how do we control how they maintain it? We train every customer’s maintenance team on our specific checklists, and we offer on-site audits whenever they want. The key maintenance steps: after every 500 cycles, they have to clean the segments with a non-abrasive solvent (no steel wool—scratches on the surface lead to uneven rubber release, which stresses the segments), and check for any minor wear on the joint edges. Once a year, we recommend disassembling the mold, inspecting each segment with a CMM, and replacing any segments that are worn more than 0.003 mm. We also send a technical rep to their plant twice a year to help with these checks, no extra cost for our long-term customers. Last year, a customer in Texas forgot to clean their mold for 800 cycles and had some wear on two segments. We went in, fixed those segments in a day, and got their production back up. They didn’t have to buy new molds, which saved them a ton of money—and us from losing a good customer.
Quality control (QC) isn’t a one-time thing at the end. It’s built into every single step. We have a team of 6 QC techs, each assigned to a specific stage: material in, machining, assembly, heat treatment, final mold testing, and even packaging. No mold leaves our shop until every single critical dimension is within our spec, which is tighter than industry standards (most ASRSM specs allow 0.01 mm error, we aim for 0.005 mm or less). We also test a “trial tire” from every new mold we ship. We send a sample to the customer along with the mold, so they can verify it meets their tire’s exact specs. If the tread depth is off, or the sidewall curvature is wrong, we adjust the segments before it ships. Last quarter, we had a customer request a custom tread pattern with a unique arc—our QC team caught that one segment was 0.004 mm off the required arc, re-machined it, and the customer told us that tire is now their top-selling model because of the perfect fit.
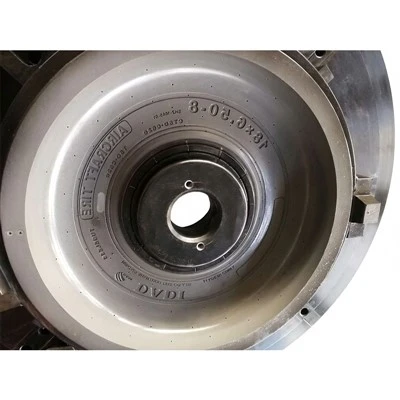
I know a lot of suppliers make accuracy sound like a mystery, but it’s just consistent, boring (in a good way) attention to detail. We don’t cut corners, we don’t rush, and we care as much about the mold’s performance as our customers do. If you’re a tire manufacturer looking for a supplier that can keep your molds accurate cycle after cycle, hit me up. We can chat, send over sample specs, or even arrange a visit to our shop so you can see the process for yourself. No sales pitches, just real talk about what makes a mold work.
Special Structure Mold References
- ASM International. (2019). Metallurgy of Tool Steels for Mold Applications. ASM Handbook, Vol. 4: Steel Heat Treating Fundamentals and Processes.
- Tire Technology International. (2022). Key Factors in Maintaining Mold Accuracy for Radial Tire Production. Tire Technology Annual Review.
- Smith, J. D. (2021). Precision Machining for Large Industrial Molds. Journal of Manufacturing Processes, Vol. 65, pp. 412-421.
- International Organization for Standardization. (2020). ISO 10919: Rubber Molds for Pneumatic Tires – Dimensions and Accuracy Requirements. ISO Standards.
Anhui Varon Mould Co., Ltd.
We are one of the most professional all-steel radial segmented molds manufacturers and suppliers in China, also support customized service. We warmly welcome you to wholesale premium all-steel radial segmented molds made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Anhui Province, Ningguo City, Economic and Technological Development Zone, Heli Industrial Park, Dongcheng Avenue
E-mail: admin@varonmould.com.cn
WebSite: https://www.wanlongmold.com/
